An intermittently bonded ribbon production system is designed to produce flexible fiber groups for contemporary, high-count cable architectures. It keeps fibers properly aligned for expedited mass fusion splicing, yet retains flexibility within the fiber group within a compact cable core.
Unlike fully bonded ribbons, intermittent bonded ribbons feature discrete bonding points at predetermined intervals. This strategic placement enables the fibers to maintain alignment while the ribbon can bend and roll into circular loose tubes and other confined spaces.
Fiber network engineers apply this technique when faced with constraints in duct space, splice closures, and equipment racks. A carefully manufactured ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.
Intermittent Bonded Ribbon Production Line
Fiber Secondary Coating Line
Fiber Ribbone Line
Key Takeaways
- A bonded ribbon production system supports compact and flexible fiber layouts.
- Separated bond points maintain optical fiber order without creating a rigid ribbon.
- Flexible ribbon structures allow manufacturers to place more fibers inside compact circular cables.
- Consistent fiber alignment makes mass fusion splicing quicker and easier.
- Ribbon technology is used across data centers, telecom routes, and optical access networks.
Intermittent Bonded Ribbon Production Line Overview
Intermittent bonded ribbon production enables the creation of fiber designs that balance compactness with usability. This method involves placing bonds at predetermined intervals, allowing for the movement of fiber subunits between these points.
This technique facilitates the incorporation of a higher number of fibers within constrained duct spaces. It also ensures the preservation of the organized ribbon structure, essential for efficient splicing and cable assembly processes.
What Is An Intermittently Bonded Fiber Ribbon?
An intermittently bonded optical fiber ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds are left flexible, enabling the ribbon to adopt various configurations without rigidification.
This configuration is often referred to as a rollable, flexible, or spider web ribbon. It diverges from the conventional flat ribbon cable, which maintains a fixed profile along its entire length.
During splicing, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers form compact bundles, optimizing space utilization within the cable.
Why High-Density Networks Use Flexible Ribbon Technology
Network designers frequently face the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure enables ribbon groups to be packed into smaller cable cores, preserving fiber order.
A fiber density ratio provides a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding can improve this ratio, allowing ribbon groups to occupy available spaces within the cable.
For installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.
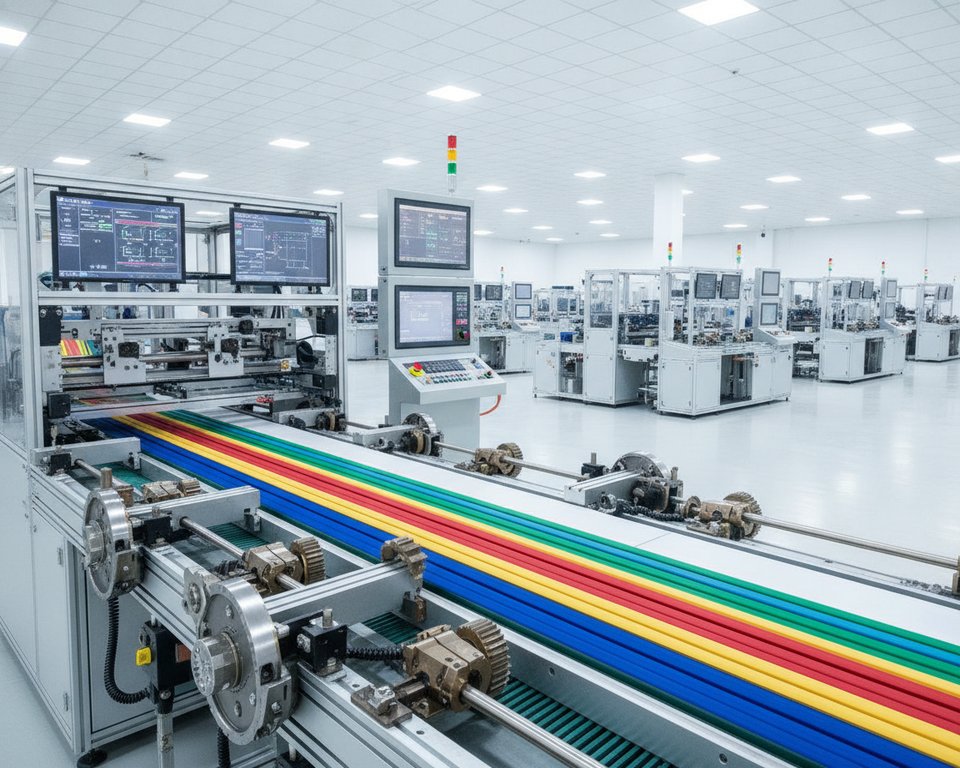 Intermittent Bonded Ribbon Production Line
| Ribbon Feature | Intermittently Bonded Design | Traditional Continuous Ribbon |
|---|---|---|
| Bond arrangement | Separated bonds at controlled intervals | Continuous bonding throughout the ribbon length |
| Fiber shape between bonds | Can curl or roll to fit compact cable spaces | Stays mainly flat and planar |
| Splicing configuration | Can be flattened for mass fusion splicing | Already held in a fixed flat ribbon form |
| Cable packing role | Enables dense placement of flexible fiber subunits | Relies on a relatively rigid ribbon stack |
| Typical cable application | Compact high-density and flexible ribbon cable structures | Traditional flat ribbon cable designs |
Intermittently Bonded Ribbon Materials And Construction
An intermittent bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture supports compact cable arrangements while allowing effortless separation during handling, routing, and splicing.
The selection of materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must maintain its fibers securely without imparting undue stiffness to the ribbon.
Fiber Count And Subunit Arrangement
Intermittently bonded ribbons can contain 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.
A 12-fiber ribbon commonly uses six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.
Controlled gaps introduced between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.
| Ribbon Construction Element | Typical Configuration | Production Purpose |
|---|---|---|
| Fiber count | 4, 8, 12, 24, or up to 36 fibers | Matches cable density and splice capacity |
| Subunit layout | Two adjacent fibers per optical fiber subunit | Maintains predictable separation between subunits |
| Fiber spacing in a subunit | Touching or up to 1.5 fiber diameters | Keeps the subunit profile compact and stable |
| Gap between subunits | Approximately 5 to 100 micrometers | Allows greater movement and flexibility near bond points |
UV-Curable Resin And Wet-On-Wet Bonding
The coating and bond systems frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.
This technique generates a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.
UV-curable resin materials can blend at the interface before curing. This encourages molecular entanglement between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.
Essential Equipment In An Intermittent Bonded Ribbon Production Line
A fiber ribbon production line combines advanced motion control with meticulous material handling. Each station ensures fibers remain aligned, clean, and stable from the initial payoff to the final winding.
The production equipment supports adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to craft a flexible custom ribbon cable, preserving the integrity of the fiber order.
Fiber Payoff With Tension Control
Payoff units deliver individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.
Within a fiber ribbon production line, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.
Discrete Bond Applicator And Coating Die
The coating system applies a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.
A discrete bond applicator then places a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.
| Equipment | Main Function | Production Benefit |
|---|---|---|
| Fiber payoff and tension unit | Feeds fibers at controlled tension | Reduces twist and uneven fiber loading |
| Subunit coating die | Creates coated optical fiber subunits | Keeps subunit dimensions and shape consistent |
| Intermittent bond applicator | Deposits resin at set intervals | Creates flexible links between adjacent subunits |
| UV curing and take-up unit | Cures and cools the ribbon before inspection and winding | Protects bond quality and preserves fiber order |
UV Curing, Cooling, And Ribbon Take-Up Equipment
UV energy cures the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.
Cooling systems reduce ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.
Ribbon winding equipment packages the finished ribbon with low, even tension. Proper winding preserves the finished bonded structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.
Fiber Preparation, Alignment, And Color Sequence Control
A stable ribbon cable begins with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.
Managing Fiber Identification During Splicing And Maintenance
A clearly defined fiber color sequence is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.
When fiber counts increase, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.
| Ribbon Fiber Position | Standard Color | Production Purpose |
|---|---|---|
| 1 | Blue | Marks the first position in the standard color order |
| 02 | Orange | Supports fast visual identification |
| 3 | Green | Supports the required planar sequence |
| 4 | Brown | Helps verify subunit placement |
| 05 | Standard slate | Provides distinct mid-sequence marking |
| 6 | White | Improves visibility during inspection |
| 07 | Standard red | Helps maintain accurate splice documentation |
| 08 | Standard black | Supports sequence identification inside splice trays |
| 9 | Yellow | Supports rapid identification during restoration work |
| 10 | Standard violet | Clearly identifies fibers near the end of the sequence |
| Position 11 | Standard rose | Helps maintain clarity in higher-count ribbon layouts |
| 12 | Aqua | Finishes the standard 12-fiber color sequence |
Preventing Fiber Twist And Uneven Tension
Payoff units and guides are instrumental in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.
Operators meticulously monitor tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.
Intermittent Bond Application And UV Curing Process
Intermittent bonding integrates fiber subunits without solidifying the ribbon into a rigid form. This method facilitates compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.
Applying Intermittent Bonds At Predetermined Intervals
Bond applicators place resin at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.
A controlled applicator deposits a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends help minimize localized stress changes when the cable bends or twists.
Creating Flexible And Strong Bond Interfaces
Wet-on-wet bonding involves applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.
The resulting gradient influences various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features enhance the cable’s resistance to peeling while facilitating separation when required.
Controlling UV Curing Performance
UV lamps must provide consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.
Production operators monitor bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.
Quality Control For Fiber Ribbon And Flexible Flat Cable Output
Verifying every flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.
Frequent quality checks are important in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.
Inspection Of Bond Spacing, Ribbon Width, And Thickness
The distance between bonding points is a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.
Quality checks are performed to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.
| Inspection Point | Inspection Requirement | Production Value |
|---|---|---|
| Fiber sequence identification | Fiber count, color sequence, and position | Helps ensure accurate splicing and maintenance |
| Bonding pattern | Bond position, interval, and connection between subunits | Maintains flexibility and fiber organization |
| Finished ribbon profile | Width, thickness, and flatness | Helps the ribbon fit handling and splicing tools |
| Finished surface quality | UV curing condition, coating coverage, and surface defects | Protects the ribbon against damage during take-up |
Mechanical And Optical Performance Testing
Mechanical assessments focus on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.
Optical testing encompasses evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.
Attenuation checks and splice-related handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.
Precision Winding, Automation, And Production Efficiency
High-efficiency ribbon production relies on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.
Production Line Synchronization And Process Data Monitoring
Automated control systems synchronize payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.
Manufacturing data records capture fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.
- Payoff tension prevents fiber stretch and slack.
- Accurate bond timing keeps discrete joints evenly spaced.
- Dimensional checks detect width or thickness deviations promptly.
- Winding data facilitates lot tracking and downstream handling.
Ribbon Winding For Downstream Cable Production
A precision cable winder helps ensure the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.
Finished ribbon structures may be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.
For custom ribbon cables, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.
| Process Area | Process Control Focus | Downstream Process Benefit |
|---|---|---|
| Fiber payoff | Consistent tension with correct fiber color order | Orderly ribbon placement during cable assembly |
| Bond application | Stable spacing with repeatable resin deposition | Consistent flexible behavior in downstream operations |
| UV curing | Controlled lamp output and exposure time | Properly cured bonds before ribbon winding |
| Cable winding system | Uniform traverse with controlled spool tension and layering | Controlled ribbon feed into loose tube or central tube production |
Applications, Splicing, And Connector Planning For Ribbon Cable
Ribbon fiber plays an important role in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.
A meticulously planned ribbon cable assembly enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.
Advantages Of Mass Fusion Splicing
Ribbon fusion equipment enables the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.
Mass fusion processing lowers handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.
Loose tube cable, by comparison necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.
Planning Connections For Dense Fiber Links
Multi-fiber connections commonly use MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.
Planning also considers transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.
| Network Planning Item | What It Determines | Common Application |
|---|---|---|
| Fiber ribbon count | Splice capacity and cassette selection | 12-fiber and 24-fiber network backbones |
| MPO or MTP multi-fiber connector | Polarity, gender, and port compatibility | Data center trunk links and 5G equipment areas |
| Multi-fiber harness or fanout assembly | Transition from multi-fiber connections to single-fiber ports | Switch ports and high-density patching areas |
| Optical link loss budget | Maximum allowable loss through connectors, splices, and cable length | High-speed fiber cable network paths |
Shanghai Weiye OFC Equipment For Fiber Ribbon Production Lines
Shanghai Weiye OFC Equipment, widely identified as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to ensure consistent processing, facilitate clear operator control, and enable seamless integration into production lines.
For manufacturers planning an intermittent bonded ribbon production line, SHWY supports every stage of ribbon handling, curing, and winding with suitable machinery.
SHWY Experience With Optical Fiber And Cable Machinery
Operating since 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.
In 2020, SHWY transitioned to independence, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.
SHWY Production Equipment Portfolio
SHWY offers a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.
For fiber ribbon manufacturing projects, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.
Additional SHWY equipment includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.
Conclusion
An intermittent bonded ribbon production line integrates fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step helps preserve fiber sequence while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.
The resultant ribbon cable supports efficient mass fusion splicing and organized fiber management. It is particularly useful for networks with high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.
Comprehensive project planning reaches beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.